
What is the milling progress?
Leave a message
What is the milling progress?
Milling is the most common form of machining, a material removal process, which can create a variety of features on a part by cutting away the unwanted material. The milling process requires a milling machine, workpiece, fixture, and cutter. The workpiece is a piece of pre-shaped material that is secured to the fixture, which itself is attached to a platform inside the milling machine. The cutter is a cutting tool with sharp teeth that is also secured in the milling machine and rotates at high speeds. By feeding the workpiece into the rotating cutter, material is cut away from this workpiece in the form of small chips to create the desired shape.

Milling is typically used to produce parts that are not axially symmetric and have many features, such as holes, slots, pockets, and even three dimensional surface contours. Parts that are fabricated completely through milling often include components that are used in limited quantities, perhaps for prototypes, such as custom designed fasteners or brackets. Another application of milling is the fabrication of tooling for other processes. For example, three-dimensional molds are typically milled. Milling is also commonly used as a secondary process to add or refine features on parts that were manufactured using a different process. Due to the high tolerances and surface finishes that milling can offer, it is ideal for adding precision features to a part whose basic shape has already been formed.

Equipment
Milling machines can be found in a variety of sizes and designs, yet they still possess the same main components that enable the workpiece to be moved in three directions relative to the tool. These components include the following:
Base and column - The base of a milling machine is simply the platform that sits on the ground and supports the machine. A large column is attached to the base and connects to the other components.
Table - The workpiece that will be milled is mounted onto a platform called the table, which typically has "T" shaped slots along its surface. The workpiece may be secured in a fixture called a vise, which is secured into the T-slots, or the workpiece can be clamped directly into these slots. The table provides the horizontal motion of the workpiece in the X-direction by sliding along a platform beneath it, called the saddle.
Saddle - The saddle is the platform that supports the table and allows its longitudinal motion. The saddle is also able to move and provides the horizontal motion of the workpiece in the Y-direction by sliding transversely along another platform called the knee.
Knee - The knee is the platform that supports the saddle and the table. In most milling machines, sometimes called column and knee milling machines, the knee provides the vertical motion (Z direction) of the workpiece. The knee can move vertically along the column, thus moving the workpiece vertically while the cutter remains stationary above it. However, in a fixed bed machine, the knee is fixed while the cutter moves vertically in order to cut the workpiece.
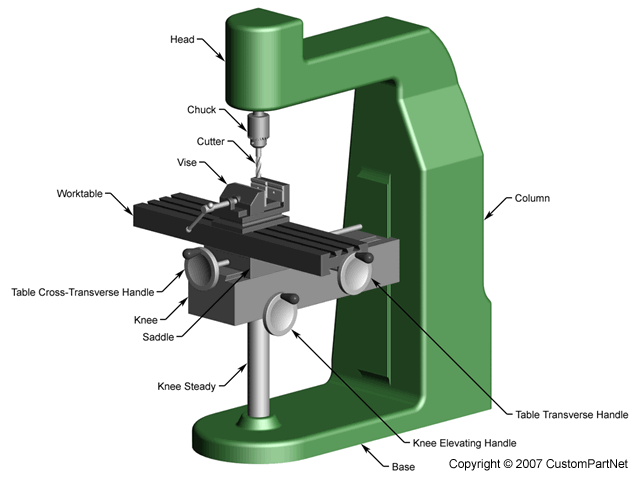
Manual vertical milling machine
The above components of the milling machine can be oriented either vertically or horizontally, creating two very distinct forms of milling machine. A horizontal milling machine uses a cutter that is mounted on a horizontal shaft, called an arbor, above the workpiece. For this reason, horizontal milling is sometimes referred to as arbor milling. The arbor is supported on one side by an overarm, which is connected to the column, and on the other side by the spindle. The spindle is driven by a motor and therefore rotates the arbor. During milling, the cutter rotates along a horizontal axis and the side of the cutter removes material from the workpiece. A vertical milling machine, on the other hand, orients the cutter vertically. The cutter is secured inside a piece called a collet, which is then attached to the vertically oriented spindle. The spindle is located inside the milling head, which is attached to the column. The milling operations performed on a vertical milling machine remove material by using both the bottom and sides of the cutter.
Milling machines can also be classified by the type of control that is used. A manual milling machine requires the operator to control the motion of the cutter during the milling operation. The operator adjusts the position of the cutter by using hand cranks that move the table, saddle, and knee. Milling machines are also able to be computer controlled, in which case they are referred to as a computer numerical control (CNC) milling machine. CNC milling machines move the workpiece and cutter based on commands that are preprogrammed and offer very high precision. The programs that are written are often called G-codes or NC-codes. Many CNC milling machines also contain another axis of motion besides the standard X-Y-Z motion. The angle of the spindle and cutter can be changed, allowing for even more complex shapes to be milled.
Tool of Milling
The tooling that is required for milling is a sharp cutter that will be rotated by the spindle. The cutter is a cylindrical tool with sharp teeth spaced around the exterior. The spaces between the teeth are called flutes and allow the material chips to move away from the workpiece. The teeth may be straight along the side of the cutter, but are more commonly arranged in a helix. The helix angle reduces the load on the teeth by distributing the forces. Also, the number of teeth on a cutter varies. A larger number of teeth will provide a better surface finish. The cutters that can be used for milling operations are highly diverse, thus allowing for the formation of a variety of features. While these cutters differ greatly in diameter, length, and by the shape of the cut they will form, they also differ based upon their orientation, whether they will be used horizontally or vertically.
A cutter that will be used in a horizontal milling machine will have the teeth extend along the entire length of the tool. The interior of the tool will be hollow so that it can be mounted onto the arbor. With this basic form, there are still many different types of cutters that can be used in horizontal milling, including those listed below.
Plane (helical) mill
Form relieved mill
Staggered tooth mill
Double angle mill
Another operation known as a straddle milling is also possible with a horizontal milling machine. This form of milling refers to the use of multiple cutters attached to the arbor and used simultaneously. Straddle milling can be used to form a complex feature with a single cut.
For vertical milling machines, the cutters take a very different form. The cutter teeth cover only a portion of the tool, while the remaining length is a smooth surface, called the shank. The shank is the section of the cutter that is secured inside the collet, for attachment to the spindle. Also, many vertical cutters are designed to cut using both the sides and the bottom of the cutter. Listed below are several common vertical cutters.
Flat end mill
Ball end mill
Chamfer mill
Face mill
Twist drill
Reamer
Tap
All cutters that are used in milling can be found in a variety of materials, which will determine the cutter's properties and the workpiece materials for which it is best suited. These properties include the cutter's hardness, toughness, and resistance to wear. The most common cutter materials that are used include the following:
High-speed steel (HSS)
Carbide
Carbon steel
Cobalt high speed steel
The material of the cutter is chosen based upon a number of factors, including the material of the workpiece, cost, and tool life. Tool life is an important characteristic that is considered when selecting a cutter, as it greatly affects the manufacturing costs. A short tool life will not only require additional tools to be purchased, but will also require time to change the tool each time it becomes too worn. The cutters listed above often have the teeth coated with a different material to provide additional wear resistance, thus extending the life of the tool. Tool wear can also be reduced by spraying a lubricant and/or coolant on the cutter and workpiece during milling. This fluid is used to reduce the temperature of the cutter, which can get quite hot during milling, and reduce the friction at the interface between the cutter and the workpiece, thus increasing the tool life. Also, by spraying a fluid during milling, higher feed rates can be used, the surface finish can be improved, and the material chips can be pushed away. Typical cutting fluids include mineral, synthetic, and water soluble oils.
Materials
In milling, the raw form of the material is a piece of stock from which the workpieces are cut. This stock is available in a variety of shapes such as flat sheets, solid bars (rectangular, cylindrical, hexagonal, etc.), hollow tubes (rectangular, cylindrical, etc.), and shaped beams (I-beams, L-beams, T-beams, etc.). Custom extrusions or existing parts such as castings or forgings are also sometimes used.
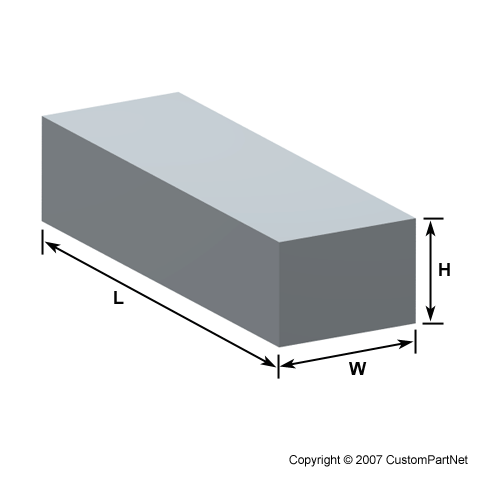 Rectangular bar |  Rectangular tube | 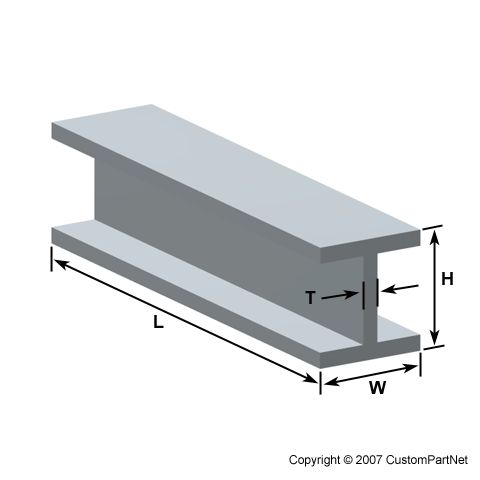 I-beam |
Milling can be performed on workpieces in variety of materials, including most metals and plastics. Common materials that are used in milling include the following:
Aluminum
Brass
Magnesium
Nickel
Steel
Thermoset plastics
Titanium
Zinc
When selecting a material, several factors must be considered, including the cost, strength, resistance to wear, and machinability. The machinability of a material is difficult to quantify, but can be said to posses the following characteristics:
Results in a good surface finish
Promotes long tool life
Requires low force and power to mill
Provides easy collection of chips